Volkswagen’s Gotion deal reveals the cost of building Europe’s LFP battery industry
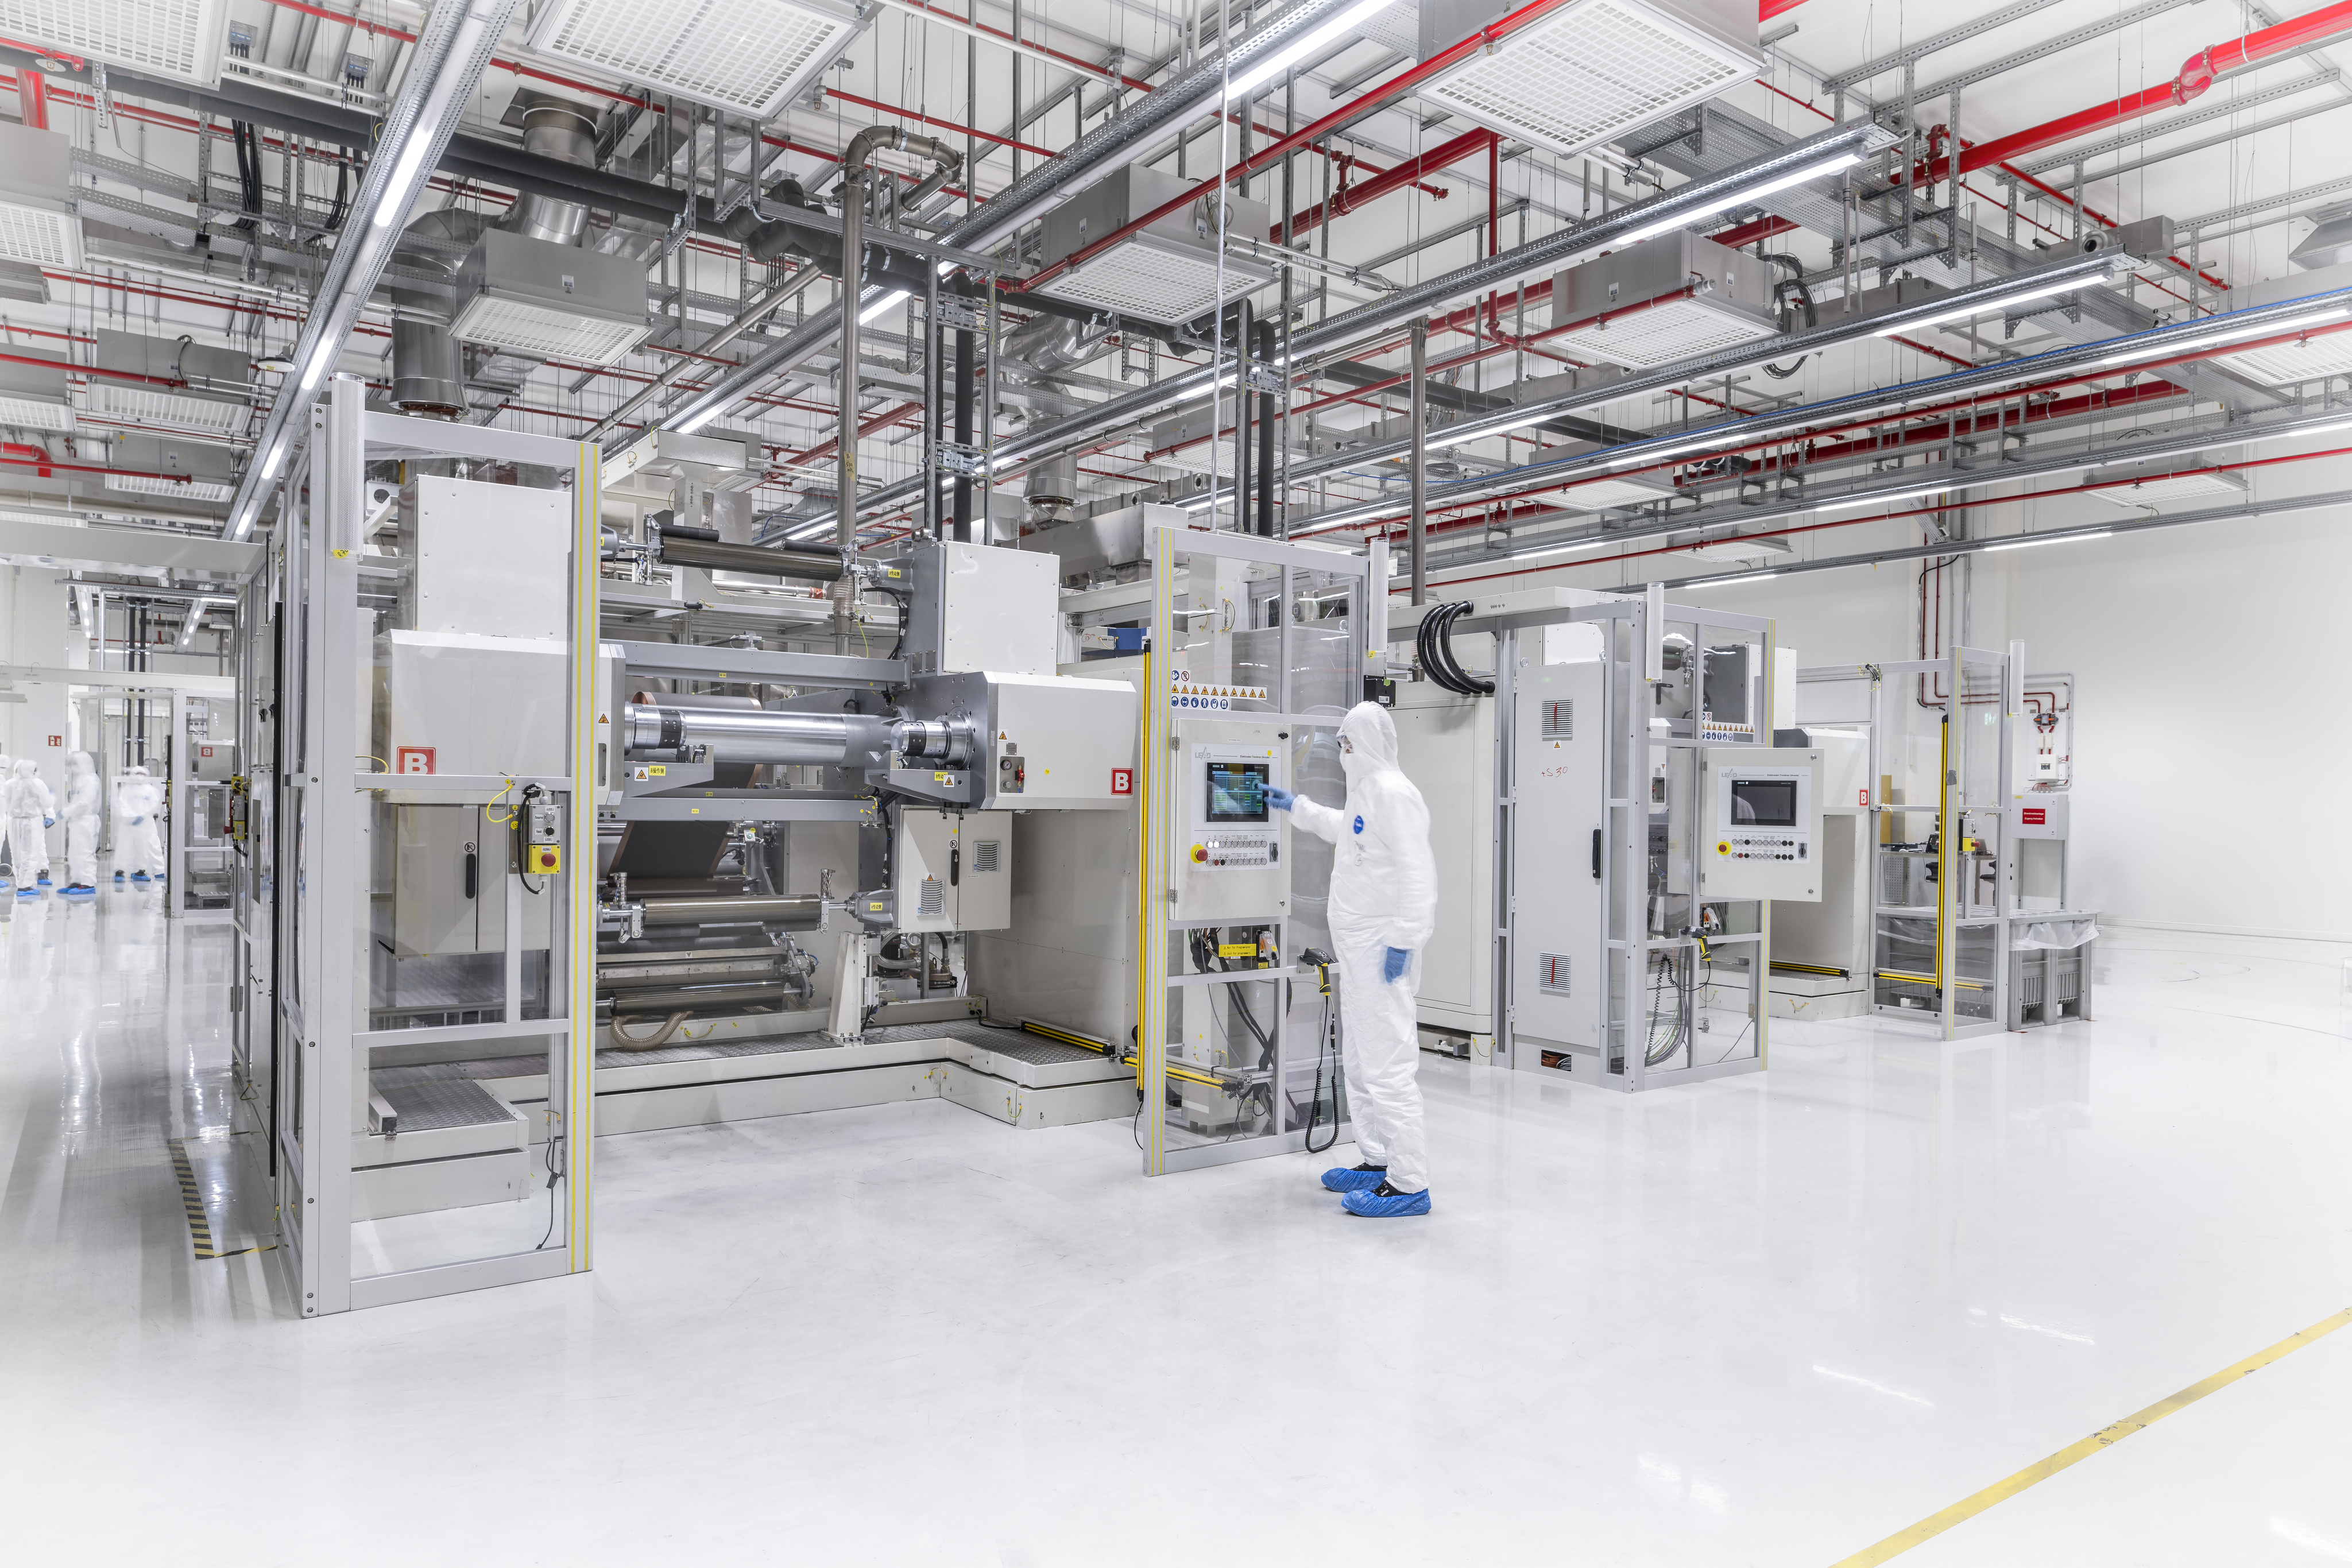
Illustrative image: Volkswagen AG
Volkswagen’s decision to bring China’s Gotion into its Valencia battery operation gives the plant additional capital, manufacturing knowledge and a defined role in the European electric vehicle market.
It also illustrates the depth of the challenge facing Europe. Establishing a cell factory is only one part of a supply chain that includes processed materials, production equipment, battery management electronics, safety systems and the knowledge needed to achieve acceptable yield at scale.
Under the agreement, Gotion will invest approximately €1.1 billion for a 49% interest in the Valencia operation. PowerCo, Volkswagen’s battery subsidiary, will retain 51% and the partners plan to manage the venture jointly.
PowerCo also expects to invest around €470 million by 2030 for 49% interests in a Gotion cell factory in Šurany, Slovakia and a proposed cathode material facility in Kenitra, Morocco.
All three transactions remain subject to regulatory approvals and customary closing conditions.
LFP changes the engineering balance
The Valencia plant is intended to become a European production centre for lithium iron phosphate cells.
LFP avoids nickel and cobalt in the cathode. Its olivine crystal structure provides strong thermal and chemical stability and the chemistry generally offers long cycle life. These characteristics make it attractive for mainstream vehicles and stationary storage.
Its lower specific energy than high nickel chemistries can impose a mass or volume penalty at pack level. Vehicle designers must balance this against lower material cost, durability and reduced thermal propagation risk.
LFP accounted for more than 55% of global electric vehicle battery deployment in 2025 according to the International Energy Agency. Its position in Europe remains much smaller: it supplied just over 10% of European Union demand and almost all of those batteries arrived from China, either as imported packs or inside imported vehicles.
Volkswagen estimates that LFP could reach between 40% and 60% of the European market by 2030. Achieving anything close to that range would create significant demand for the electronics surrounding the cells.
State of charge is harder to observe
LFP’s relatively flat open circuit voltage curve through much of its operating range creates a specific battery management challenge.
With some cell chemistries, terminal voltage provides a useful indication of state of charge. Across the LFP plateau, a small voltage difference can correspond to a much larger change in remaining capacity.
Voltage measurement noise, analogue to digital converter resolution, temperature and calibration error therefore have a material effect on the estimate. LFP also exhibits hysteresis, meaning the observed voltage can depend on whether the cell has recently been charged or discharged.
Coulomb counting measures current over time but accumulates errors from sensor offset, timing and uncertainty in the cell’s usable capacity. That capacity also changes with temperature and ageing.
A practical battery management system combines current integration with cell voltage, temperature and a model of the battery’s behaviour. Extended or unscented Kalman filters are commonly investigated for this purpose while newer approaches combine physical models with adaptive or learned correction.
Recent research has focused on changing the estimator’s weighting according to the information available from the voltage measurement. When the cell is operating on the flat part of the curve, the algorithm can reduce its reliance on voltage based correction and account more explicitly for hysteresis and current sensor bias.
This increases requirements for current sensing accuracy, low drift analogue front ends and careful characterisation across temperature and cell age. The algorithm cannot compensate indefinitely for poor measurement data.
Monitoring a high voltage series stack
An automotive pack may contain many cells connected in series. Small differences in capacity, impedance and self discharge cause their state of charge to diverge over time.
Cell monitoring devices measure individual cell voltages and temperatures while communicating across a stack that can operate at several hundred volts. The design requires accurate analogue conversion, high common mode tolerance and galvanic isolation between the high voltage battery domain and the vehicle’s low voltage control network.
Monitoring devices are often connected through isolated daisy chains to reduce wiring and allow fault detection across the stack. Communications integrity matters because a missed or corrupted measurement can conceal a developing overvoltage or thermal condition.
Passive balancing dissipates energy from higher charged cells through resistors. Active balancing moves energy between cells or modules but adds conversion stages, switching devices and control complexity.
The preferred approach depends on cell consistency, pack size, cost and how much usable capacity the vehicle manufacturer is prepared to sacrifice to the weakest cell.
Safety extends beyond the monitoring IC
The battery management controller must identify overvoltage, undervoltage, excessive current, insulation faults and abnormal temperature gradients.
High voltage contactors disconnect the pack during a serious fault. A precharge circuit limits inrush current when connecting the battery to the vehicle’s DC link capacitors. Pyrotechnic disconnects can provide rapid physical isolation following a crash or severe electrical event.
Insulation monitoring detects leakage between the high voltage system and the vehicle chassis. Current sensors support state estimation and protection while temperature sensing helps identify local faults before they propagate.
These functions must be designed as a coordinated safety architecture. Redundant measurements only add value if they do not share a failure mode that can invalidate both channels.
The selection of cells consequently affects the complete pack design. LFP’s thermal stability may reduce some risks but it does not remove the need for fault detection, isolation and controlled shutdown.
Manufacturing yield is the industrial test
A factory’s nameplate capacity says little about the number of automotive grade cells it can deliver consistently.
Cell production requires uniform electrode slurry, coating thickness, drying, calendaring and electrolyte filling. Moisture and particulate contamination can create latent defects. Misalignment or burrs introduced during cutting and assembly can increase the risk of an internal short circuit.
Formation cycling creates the initial interphase inside the cell and is both energy intensive and time consuming. Electrical measurements collected during formation and ageing can identify abnormal leakage, capacity or impedance before the cell enters a vehicle pack.
This places significant demands on programmable power conversion, high channel count measurement, calibration and manufacturing data systems. Machine vision and traceability must connect a finished cell with its material batches, process parameters and test history.
For European equipment and component suppliers, this may be the more immediate opportunity. A large cell plant requires power supplies, precision measurement, motion control, sensing, industrial communications and automated inspection at considerable scale.
Local production does not guarantee a local supply chain
The IEA estimates that China accounted for more than 80% of battery cell production in 2025, about 85% of cathode active material and more than 90% of anode active material.
The agency also says LFP cathode material and precursor production remains almost entirely concentrated in China, together with much of the associated technical expertise.
Gotion is therefore contributing process knowledge and access to an established industrial network as well as capital.
That should reduce Volkswagen’s execution risk. It also means European production will initially depend on technology and upstream capacity that Europe is attempting to localise.
The Moroccan cathode material venture addresses part of this problem. Its value will depend on where precursor materials, production equipment and intellectual property originate and whether the resulting material can meet automotive consistency requirements at a competitive price.
What the deal changes
The partnership improves Volkswagen’s prospects of bringing affordable LFP cells into European vehicle programmes. It also gives Gotion a substantial position inside Europe’s automotive manufacturing base.
The technical measure of success will extend beyond cost per kilowatt hour. PowerCo will need to demonstrate production yield, cell consistency, predictable ageing and traceability across high volumes.
At pack level, the electronics must extract usable capacity from a chemistry whose state of charge is comparatively difficult to observe. That requires accurate sensing, robust estimation and a safety architecture able to detect faults across a large series stack.
For Europe’s electronics industry, the opportunity lies in the layers around the cell: monitoring, isolation, power conversion, automation, inspection and production test.
Whether that value remains in Europe will depend on the sourcing decisions taken before the Valencia lines enter volume production. Building the factory establishes capacity. Localising its component, equipment and engineering base would establish an industry.